


Role of material selection in mix optimization of 3D printable concrete
ABSTRACT. The printing process is a novel digitally-controlled additive manufacturing method which can build architectural and structural components without formwork, unlike conventional concrete construction methods. The most important fresh properties are extrudability and buildability, which have mutual relationships with workability and open time. These properties are greatly influenced by the mix proportions and the presence of superplasticiser, retarder, accelerator and polypropylene fibres. The present study is about optimisation of material quantity to obtain a 3D printable mix with 3D printer. Cement, fly ash, silica fume, fine aggregate, water and chemical admixture are used for developing a 3D printable mix and optimum dose of chemical admixture such as PC base chemical admixture and Viscosity Modifying Admixture (VMA) is used to optimise the 3D printable mix. The study indicated that the dosage of superplasticizer needed to achieve the similar flow value increases as a/b increases. The plastic viscosity increased by about 35 % when a/b increased from 0.75 to 0.9. The flow was ranging from 160 to 225 mm which indicates dependency on the material type and packing density. Study also highlighted that yield stress of mix is important to achieve buildability and low yield stress value can lead to collapse of layers and will also prevent layer wise buildability. The optimum dose of polypropylene fibre was found to be 0.1 % to achieve 3D printable mix without clogging or shrinkage crack. The open time is found to be about 12—15 minutes for the materials. Studies reported in this paper highlights that both mix optimisation with different combination of cementitious binders and selection of optimum dosage of superplasticizer and VMA are very critical in achieving a 3D printable concrete.
Keywords: 3D printing, concrete mix, flow, buildability, yield stress, open time.
1. Introduction
Concrete is generally placed into formwork and then vibrated to fabricate structural components. Two alternative construction strategies namely self-compacting and sprayed concretes have been developed to eliminate the compaction process. 3D concrete printing is a latest technology that shows great potential with respect to the increase of productivity and safety in construction [1—4]. Based on past research, it is seen that economically feasible concrete printing approaches are based on layered extrusion. In this context, 3D printable concrete is a “tailor-made” material which can be delivered by the pumping system and extruded through the nozzle of a 3D printer. Then, after its deposition, it maintains its shape stable under the gravitational load of subsequent printed concrete layers without the requirement of formwork. Compared to conventional concrete, 3D printable mix, is a novel, automatic, digital technology which brings numerous benefits to construction, like highly flexible architectural design, formwork-free fabrication, faster construction, material savings, etc. [5—6]. Contour crafting method is globally used in 3D printing as it is uses systematic deposition of material as directed by 3D model from printer. Any complex shape can be made by 3D printing, if control can be made on the behaviour of printed material. The rheological properties of printed concrete are most critical in 3D printing of any object. Similarly, the mix design and its compatibility with printing parameter are equally important. The 3D printable mix requires a flowable consistency until it remains in printing nozzle while its requirement gets changed from a flowable mix to plastic mix which remain plastic until next layer get print and after that it must gain sufficient yield stress that can bear the weight of successive printed layers [5—6]. The mix design and its optimisation plays an imported role in successful printing of 3D printable objects. The optimum water content and dose of chemical admixture maintain the flow in the mix while the optimum ratio of cementitious materials and fine aggregate content gives an optimum density which gets pumped through pipe and nozzle and gives a printable mix without compaction for a layer by layer print. Jun Ho Jo et.al [7] developed a 3D printer for concrete structures for testing of cementitious materials for laboratory testing purpose. They developed a concrete 3D printer 1m × 1m × 1m for different design mixes to find their suitability and efficacy for the developed of 3D printable mortar. Jia Chao Lin et.al. [8] studied the effect of Processing Parameters on 3D Printing of Cement — based Materials and concluded that in 3D printing with cement-based materials, the material properties and process parameters have a great impact on the printing process. They showed that the best single-layer height and nozzle diameter ratio are between 0.4—0.6. The best parameters for the equipment are (a) output displacement is 9 · 10–2 m3/h, (b) printing speed should be controlled in 4—8 cm/s. At the same time, 3D printing should try to choose a shorter length of the pipeline, and ensure that the pipeline should be straight to avoid the pipe bending and suspension. The prevalent processes of 3D printing are Extrusion-based printing, Binder jetting, Mesh mould approach (cutting and welding) etc. The additive process in construction with automation is further developed by Khoshnevis [4]. Among all the processes, the most widely used method is the Extrusion-based printing (Fig. 1).
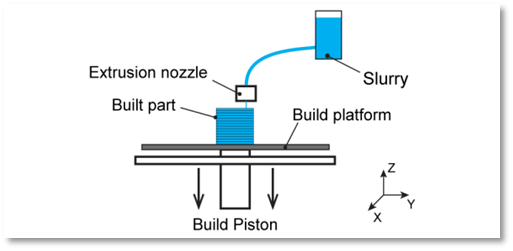
Fig. 1. Schematic diagram of Extrusion based printing [4]
A critical issue in 3D printable mix is the selection of raw materials and the mix design so as to meet the pumpability, extrudability and buildability which are key process-related material characteristics required for a successful 3D concrete printing. These characteristics are beyond the general requirements to concrete as described in codes and guidelines by consistency classes and corresponding workability testing. There are some empirical mix design methods for 3D printable mix which have been suggested by past researchers [9] but there are still no commonly accepted mix design methods. Set of trial experiments done in past has indicated a flow value of 50—60 % suitable for designing the printable mixtures. Similar flow values are reported in the literature for printable concrete [10—15]. The rheological measurements with granular suspensions like cementitious mixtures are prone to effects like particle migrations and solvent drying. These factors may have an influence on the results and are some of the limitations on performing rheological measurements with cement-based materials [14—15]. While a highly workable material is needed for 3D concrete printing to ensure easy transportability (usually by pumping) to the printing head, the extruded material is required to be relatively stiff to ensure that the deposited filaments retain their shape [16]. Nozzles of various orifice shapes such as rectangular, square, circular and elliptical are in use. The nozzle orifice shape may be chosen as per the intended use. Circular nozzles offer ease of printing at corners or changes in angle of the structure to be printed. But the lesser contact area between extruded beads may affect the stability of layers [17]. In 3D printing, buildability is a challenging material issue and to overcome it, the freshly extruded material should regain its initial viscosity and yield stress prior to the deposition of the next layer over it Layer deformations may cause instability [18—20].
There are numerous factors which affect the printability of concrete simultaneously, it still can be briefly inferred that increasing the volume fraction of solid phase (including aggregate and fiber) and reducing the paste volume are beneficial for the buildability but may compromise the pumpability and extrudability of 3D printable mix. The influences of paste volume in concrete system could be inversely applied for volume of aggregates. Increasing aggregate volume fraction enhances the required pumping pressures [21—22], due to the increase in viscosity. Usage of coarse aggregates significantly influences the pumpability and extrudability of the 3D printable mix. If a particular maximum aggregate size is critical or not is dependent on the pump and print head setup, especially the nozzle diameter. Pozzolanic cementitious materials with combination of fly ash and silica fume, can mitigate cold joints and the variation of overall strength to a great extent in 3D printable mix, which can be attributed to less pore and the formation of denser microstructure at the layer-interface. However, this effect also depends on the moisture in the concrete system for the further pozzolanic reaction of these materials [23—27]. It should be understood that 3D printing technology will have a limitation to the selection of some parameters in mix design, such as the size of aggregate and the type of fiber, which will further impact the mechanical, time dependent and durability property of concrete mix. In principle, materials (thixotropic) with high (static) yield stress and low viscosity, are suitable for concrete printing application. The studies have indicated that the paste to aggregate ratio has a great impact on the printability of 3D concrete. However, defects and weak interlayer surfaces can be seen in the printed specimen, resulting in a significant reduction in the mechanical performance of the printed specimen when compared with the cast concrete depending upon aggregate content [23—29]. Different from the densely packed structure of conventional cast concrete, 3D printed concrete needs more paste to coat and cover the aggregates so that the aggregates can be suspended in the paste to ensure the extrudability requirement. However, too much paste other way creates a decrease in buildability [24—30].
The aim of this study is to present the mix design concepts of 3D printable concrete mix. The present study is about optimisation of material quantity to obtain a 3D printable mix with 3D printer. Cement, fly ash, silica fume, fine aggregate, water and chemical admixture are used for develop a 3D printable mix and optimum dose of chemical admixture is used to optimise the 3D printable mix.
2. Materials
Commercially available Ordinary Portland Cement (OPC) of 43 grade conforming to the physical and chemical requirements of IS 269 has been used as the main binder in all the concrete mixes. Mineral admixtures such as Fly Ash (FA) conforming to requirements of IS 3812 (Part 1) and Silica Fume (SF) confirming to IS 15388 [33] have been incorporated in different combinations and proportions to make various binary and ternary concrete mixes. The physical properties and chemical composition of these materials are given in Table 1 & Table 2. Fine aggregates (crushed fine aggregates of zone III as per IS 383) conforming to requirements of IS 383 were used as fine aggregates. Polycarboxylate ether (PCE) based super-plasticizer conforming to IS 9103 and Viscosity Modifying Admixture (VMA) was used.
Table 1
Physical properties of OPC and mineral admixtures
| Properties | Cement | Fly Ash | Silica Fume |
| Fineness (m2/kg) | 323 | 334 | 1670 |
| Specific Gravity | 3.15 | 2.19 | 2.28 |
Table 2
Chemical composition of OPC and mineral admixtures, %
| OPC 43 | Fly Ash | Silica Fume | |
| Loss of Ignition (LOI) | 2.30 | 3.64 | 2.73 |
| Silica (SiO2) | 20.71 | 62.53 | 85.03 |
| Aluminum oxide (Al2O3) | 5.15 | 23.58 | – |
| Calcium oxide (CaO) | 59.96 | 1.17 | – |
| Magnesium oxide (MgO) | 4.57 | 0.50 | – |
| Alkalis |
|
|
|
| Na2O | 0.42 | 1.23 | 0.73 |
| K2O | 0.56 | – | 2.96 |
| Chlorides |
0.012 |
– | – |
| Insoluble Residue (IR) |
1.25 |
91.92 | – |
3. Experimental plan
Based on the past studies, an experiment plan is prepared for studying fresh properties of 3D printable concrete. OPC 43 grade Cement, fly ash, silica fume, fine aggregate (<2.36 mm), water, PC base chemical admixture and Viscosity Modifying Admixture (VMA) were used to develop a 3D printable concrete mortar. Due to different principles and printing process, 3D printing equipment cannot be universal in different areas, but the equipment operating principle is relatively consistent. The following parameter (Table 3) of customized 3D printer were fixed for development of 3D printable concrete. Provision of Two arrangement for liquid additive mixing nozzle shaft with injection control rate by software was kept. Based on literature review and customized 3D printer parameters, the following materials ranges (Table 4) were considered for development of 3D printable concrete.
Table 3
Details of customized 3D printer
| S. No. | Parameter | Range |
| 1 | Print size | 0.5—1.0 m |
| 2 | Nozzle moving speed | 0.010—0.050 m/s |
| 3 | Discharge rate | 0.050—0.100 M3/min. |
| 4 | Layer width | 25 mm |
| 5 | Layer height | 10—15 mm |
Table 4
Materials ranges considered for development of 3D printable mortar
| Sl. No. | Material | Range of use |
| 1 | MSA | 2.36 mm |
| 2 | Total cementitious material | 800—1100 Kg/m3 |
| 3 | OPC 43 grade cement | 300—600 Kg/m3 |
| 4 | Flyash | 300—500 Kg/m3 |
| 5 | Silica fume | 50—135 Kg/m3 |
| 6 | Water | 250—330 Kg/m3 |
| 7 | Chemical Admixture PC base | 0.1—0.5 (% by mass of total cementitious) |
| 8 | Viscosity Modifying Agent | 0.05—0.20 (% by mass of total cementitious) |
4. Mix design details
In order to optimize the mix, more than 30 trials were done and six mixes with following proportions (Table 5) were prepared and flow, extrudability, printability and buildability were tested for all the mixes. Mixing was done in a pan type mixer attached to 3D printer setup. Initially dry mixing of fine aggregate and cementitious materials was done for two minutes. After that water was added with superplasticizer. The mixing was stopped after two minutes and further VMA was added and mixing was continued for two minutes. From a set of trial experiments, a print flow value of 70—80 % was found to be suitable for designing the printable mixtures. Similar flow values are reported in the literature [19—21] for printable concrete. The aggregate-to-binder ratio (a/b) was kept in range from 0.75 to 0.9 and the dosage of superplasticizer was adjusted to achieve a flow value in the range of 60—80 %. A nominal VMA dosage in range of 0.05 % to 0.1 % of the binder was used for all the mixtures. The dosage of superplasticizer needed to achieve the similar flow value increases as a/b increases. This is due to the reduced water content in the mixtures with higher a/b. The flow of mix was measured by flow table as procedure given in IS: 1727—1967. The range of flow in mm was 160 to 225 mm.
Table 5
Mix details of 3D printable concrete
|
Sl. No. |
Cement kg/m3 | Fly Ash kg/m3 | Silica Fume kg/m3 | PC Admixture | VMA | Water kg/m3 | Polypropylene fibers % by volume of concrete | Fine Aggregate |
| Percentage by cementitious | Weight of materials | |||||||
| Mix 1 | 300 | 600 | 100 | 0.25 | 0.10 | 320 | – | 900 |
| Mix 2 | 300 | 600 | 100 | 0.17 | 0.05 | 280 |
– |
832 |
| Mix 3 | 225 | 540 | 135 | 0.15 | 0.07 | 290 |
– |
750 |
| Mix 4 | 300 | 600 | 75 | 0.14 | 0.06 | 295 |
– |
730 |
| Mix 5 | 400 | 500 | 100 | 0.20 | 0.10 | 295 | 0.10 % (1.00 kg) | 825 |
| Mix 6 | 400 | 500 | 100 | 0.22 | 0.08 | 295 | 0.25 % (2.5 kg) | 825 |
The appropriate way to design compositions with high paste volume is to use additives as replacement of Portland cement. The plastic viscosity increases by 35 % when a/b increased from 0.75 to 0.9. This increasing trend in plastic viscosity can be explained by the Krieger-Dougherty model [21]. Few trials were also done with Polypropylene (PP) fibers. The length and thickness of the fibers were 12 mm and 40 µm respectively. The range of compressive strength for the mixes was between 45—55 MPa. If volume of paste is enhanced by increasing cement content or with another fast reacting binder, then buildability is expected to improve with paste volume. In contrast, if the paste volume is enhanced by adding inert or slow reacting additives, then buildability may remain the same or sometimes it decreases. As far as the parameters in the mix design of 3D printed concrete are to be taken care, it is to be noted that the choice of mix constituents and their proportions depends upon features of 3D printing technology applied, as indicated in Fig. 2. 3D printed concrete have high binder content in order to achieve the extrudability. The absence of coarse aggregate and excessively high binder content leads to higher plastic, autogenous and drying shrinkage, and as a subsequently lead to a higher probability to cracking. To mitigate the shrinkage induced cracking of 3D printed concrete, the addition of fiber has become a solution.
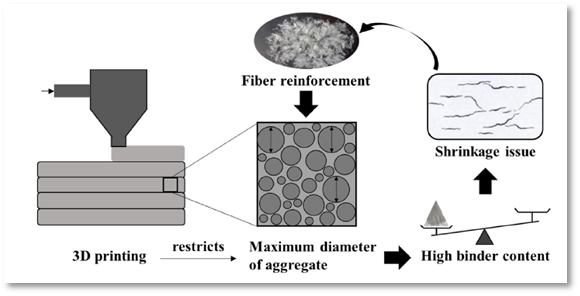
Fig. 2. Limitation in parameters for mix design for 3D printing technology [31, 32, 33]
5. Results and discussion
It was seen that extrudability and buildability depends on various factors but to reduce the complexity in mix design, the consistency / flow of trial mix was altered by adjusting the superplasticizer dosage. The concrete mix was found pumpable and continuously extrudable from 25 mm nozzle size. The printing was done with optimised concrete mix‑4 for nine layers with 0.225 metre height. The circle printed with this concrete was found stable and retained its shape till final layer of printing. Printing speed of the nozzle of 3D printer was kept as 2 cm/sec.
In few trials of 9 layers of 25 mm each, shrinkage cracks was noticed in the previously printed objects, further experiments were performed by adding Polypropylene fiber in concrete mix so that cracking can be avoided in 3D printed objects and stability gets improved. The Polypropylene fiber were added in varying amounts of 0.1 % and 0.25 % by volume of concrete (refer table‑5). Although the mix designs achieved the optimum flow spread value for dispensing and layering of the materials, the screw inside of the nozzle compartment malfunctioned and got choked when the concrete contained more than 0.1 % of PVA fibers. The mix design with 0.1 % PVA fiber did not cause clogging in the nozzle compartment. Therefore, the optimum ratio is found to be 0.1 % of the fiber that print material without clogging or shrinkage crack.
Past studies has indicated that higher printing speed will have an impact on single layer stack stability. Superplasticizer dosage in range of 0.10 % to 0.25 % gave continuous extrusion of material without blockages in this study. Past study by Rahul et.al. [10—11] also suggested that above 0.10 % superplasticizer dosage continuous extrusion of material was possible without blockages. The width and thickness of the extruded layer conformed with dimensions of nozzle leading to “passing” in extrudability test. There was no deformation of bottom layer when it is checked for more than eight layers (figure 3) for superplasticizer dosage of 0.10 %. However, on further increasing superplasticizer dosage to 0.15 %, there was a 5 mm compression of the bottom layer. With a lower superplasticizer dosage, the yield stress were increasing as VMA dose increases allowing extrudability, whereas flow was not giving definite trend & was ranging from 160 to 225 mm which indicates dependency on the material type and packing density. Static yield stress is defined as the maximum stress which is needed to make the material flow from its state of rest. Below the yield stress, the material exhibits elastic behavior and does not flow. The static yield stress of printable concrete is measured of above mixes with the help of Vane Shear apparatus. The initial obtained shear stress of printable mix is given in Table 6. The influence of superplasticizers on the viscosity has been investigated before by past researchers [10—15], and there exists a general agreement on the fact that, although superplasticizers decrease the yield stress, it does not decrease the viscosity of the cementitious mixtures significantly. It was seen that the increase in yield stress with increase in a/b is not significant as compared to the increase observed for the plastic viscosity. High (more than 50 %) paste volume and low (less than 50 %) dosage of aggregates enables better pumpability and extrudability at a constant concrete consistency.
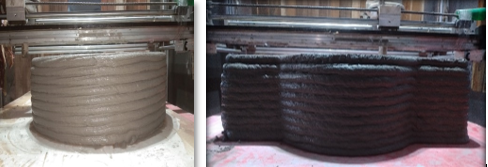
Fig. 3. Printed object using optimized concrete mix
Table 6
Flow measurements and yield stress of 3D printable mortar
| Sl. No. | Mix | Initial static yield stress (kPa) | Open Time (minutes) |
| 1 | Mix 1 | 1.72 | 15 |
| 2 | Mix 2 | 1.80 | 14 |
| 3 | Mix 3 |
1.78 |
14 |
| 4 | Mix 4 | 1.84 | 14 |
| 5 | Mix 5 |
2.23 |
13 |
| 6 | Mix 6 |
2.15 |
12 |
It was seen that the material was not extrudable after average 12—15 minutes when the material reached its open time limit. It was difficult to print the materials after this limit. However, the open time can be controlled by adding the dosage of superplasticizer suitably in the mix. For the specimen with average of 12—15 minutes of the time interval, the layers were well bonded together. However, only the surfaces exposed to the air are bonded while boundary lines of each layer is observed for the specimen with average 20 min of the time interval for the mix‑1 to mix‑6. The cross section for 40 minutes of the time interval showed each layer as a separate entity. It was observed that the boundary line became more noticeable as the time interval increased. Based on this, the maximum time gap required between printing layers was found to be average 12 minutes. The extruded layer should have a short time gap before the subsequent layer of concrete is deposited on top of previous layer. This is needed, so that the layers can maintain sufficient chemical activity and plasticity to adhere with the next layer. Otherwise, the finite ‘‘waiting time” between layers can lead to formation of cold joints. The yield stress of fresh concrete is the critical parameter which determines the shape stability. Yield stress increases over time in absence of agitation and shear stress. This is due to the nucleation of cement grains at their contact point by C-S-H formation during the dormant period before the setting initiates.
6. Conclusion
Laboratory scale customized 3D printer developed in this study indicates that the prototype printer would only be useful to optimize motion control of the machine, to study the material properties of the printed objects, and to understand the dispensing mechanism. However, design for industrial application will need to establish a relationship between screw speed and feed rate, to avoid defects such as discontinuity and clogging. The dosage of superplasticizer needed to achieve the similar flow value increases as a/b increases. This is due to the reduced water content in the mixtures with higher a/b (aggregate to binder ratio). The plastic viscosity increased by about 35 % when a/b increased from 0.75 to 0.9. With a lower superplasticizer dosage, the yield stress increases with increase in VMA dose allowing extrudability, whereas flow does not gave definite trend. The flow was ranging from 160 to 225 mm which indicates dependency on the material type and packing density. Yield stress of mix is important to achieve buildability. Low yield stress value can lead to collapse of layers and will also prevent layer wise buildability. The optimum dose of polypropylene fibre was found to be 0.1 % by volume of concrete to achieve 3D printable mix without clogging or shrinkage crack. The open time is found to be about 12—15 minutes for the materials. A fresh mix of the material was prepared after 15 minutes considering its open time and maximum time interval between printing layers. Studies highlighted that both mix optimisation with different combination of cementitious binders and selection of optimum dosage of superplasticizer and VMA are very critical in achieving a 3D printable concrete.
3D printable concrete mixes adopted in recent years are with high amounts of cementitious binder and low amounts of aggregates which makes them prone to shrinkage cracking and poor durability. This is not in line with the principle of sustainability and durability. Therefore, investigating the application of 3D printable concrete with coarse aggregate and low binder contents is important in matching the goal of sustainable construction.
REFERENCES
1. Khoshnevis, B.; Hwang, D.; Yao, K.-T.; Zhenghao, Y. Mega-scale fabrication by contour crafting. Int. J. Ind. Syst. Eng. 2006, 1.
2. Khoshnevis, B. Automated construction by contour crafting — related robotics and information technologies. Autom. Constr. 2004, 13, 5—19.
3. Bos, F., Wolfs, R.; Ahmed, Z.; Salet, T. Additive manufacturing of concrete in construction: Potentials and challenges of 3D concrete printing. Virtual Phys. Prototype. 2016, 11, 209—225
4. Wangler, T.; Lloret, E.; Reiter, L.; Hack, N.; Gramazio, F.; Kohler, M.; Bernhard, M.; Dillenburger, B.; Buchli, J.; Roussel, N.; et al. Digital Concrete: Opportunities and Challenges. RILEM Lett. 2016, 1, 67—75.
5. Khoshnevis, B.; Hwang, D. Contour Crafting. In Rapid Prototyping: Theory and Practice; Kamrani, A., Nasr, E.A., Eds.; Springer: Boston, MA, USA, 2006; pp. 221—251, ISBN 978-0-387-23291-1.
6. Khoshnevis, B.; Bukkapatnam, S.; Kwon, H.; Saito, J. Experimental investigation of contour crafting using ceramic materials. Rapid Prototype. J. 2001, 7, 32—41.
7. Jo, J.H., Jo, B.W., Cho, W. et al. Development of a 3D Printer for Concrete Structures: Laboratory Testing of Cementitious Materials. Int J Concr Struct Mater 14, 13 2020.
8. Jia Chao LIN, Jun WANG, Xiong WU, Wen YANG, Ri Xu ZHAO, Ming BAO, Effect of Processing Parameters on 3D Printing of Cement — based Materials, E 3S Web of Conferences 38, 03008, 2018.
9. Chao Zhang, Venkatesh Naidu Nerella, Anurag Krishna, Shen Wang, Yamei Zhang, Viktor Mechtcherine, Nemkumar Banthia, Mix design concepts for 3D printable concrete: A review, Cement and Concrete Composites, Volume 122, 2021, 104155.
10. A.V. Rahul, M. Santhanam, H. Meena, Z. Ghani, 3D printable concrete: mixture design and test methods, Cem. Concr. Compos. 97 (2018) 13—23.
11. A.V. Rahul, A. Sharma, M. Santhanam, A desorptivity-based approach for the assessment of phase separation during extrusion of cementitious materials, Cem.Concr. Compos. 108 (2020) 103546.
12. Z. Liu, M. Li, Y. Weng, T.N. Wong, M.J. Tan, Mixture design approach to optimize the rheological properties of the material used in 3D cementitious material printing, Constr. Build. Mater. 198 (2018) 245—255.
13. G. Ma, N.M. Salman, L. Wang, F. Wang, A novel additive mortar leveraging internal curing for enhancing interlayer bonding of cementitious composite for 3D printing, Constr. Build. Mater. 244 (2020) 118305.
14. Y.W.D. Tay, Y. Qian, M.J. Tan, Printability region for 3D concrete printing using slump and slump flow test, Compos. Part B Eng. 174 (2019) 106968.
15. S.C. Paul, Y.W.D. Tay, B. Panda, M.J. Tan, Fresh & hardened properties of 3D printable cementitious materials for building and construction, Arch. Civ. Mech. Eng. 18 (2018) 311—319.
16. T.T. Le, S.A. Austin, S. Lim, R.A. Buswell, R. Law, A.G.F. Gibb, T. Thorpe, Hardened properties of high-performance printing concrete, Cement Concr. Res. 42 (3) (2012) 558—566.
17. T.T. Le, S.A. Austin, S. Lim, R.A. Buswell, A.G.F. Gibb, T. Thorpe, Mix design and fresh properties for high-performance printing concrete, Mater. Struct. 45 (8) (2012) 1221—1232.
18. J. Kruger, S. Cho, S. Zeranka, C. Viljoen, G. van Zijl, 3D concrete printer parameter optimisation for high rate digital construction avoiding plastic collapse, Compos. Pt. B Eng. 183 (2020) 107660.
19. V.C. Li, F.P. Bos, K. Yu, W. McGee, T.Y. Ng, S.C. Figueiredo, K. Nefs, V. Mechtcherine, V.N. Nerella, J. Pan, G.P.A.G. van Zijl, P.J. Kruger, On the emergence of 3D printable engineered, strain hardening cementitious composites (ECC/SHCC), Cement Concr. Res. 132 (2020) 106038.
20. H. Ogura, V.N. Nerella, V. Mechtcherine, Developing and testing of the strain hardening cement-based composites (SHCC) in the context of 3D‑printing, Materials 11 (8) (2018), 18.
21. I.M. Krieger, T.J. Dougherty, A mechanism for non-Newtonian flow in suspensions of rigid spheres, Trans. Soc. Rheol. 3 (1959) 137—152.
22. M.K. Mohan, A.V. Rahul, K. Van Tittelboom, G. De Schutter, Evaluating the Influence of Aggregate Content on Pumpability of 3D Printable Concrete, RILEM Book series, 2020, pp. 333—341.
23. V.N. Nerella, M. Nather, A. Iqbal, M. Butler, V. Mechtcherine, Inline quantification of extrudability of cementitious materials for digital construction, Cement Concr. Compos. 95 (2019) 260—270.
24. J. Kruger, S. Zeranka, G. van Zijl, A rheology-based quasi-static shape retention model for digitally fabricated concrete, Construct. Build. Mater. 254 (2020) 119241.
25. Ojha, P. N., Mittal, P., Singh, A., Singh, B., and Arora, V. V., “Optimization and evaluation of ultra-high-performance concrete,” Journal of Asian Concrete Federation, vol. 6, no. 1. Asian Concrete Federation, pp. 26—36, Jun. 30, 2020.
26. Arora V V., Singh B, (2016), Durability Studies on Prestressed Concrete made with Portland Pozzolana Cement, Indian Concrete Journal, Vol.90, No.8, 41—48, August, 2016.
27. V Patel, B. Singh, and V. V Arora, “Study on fracture behaviour of high strength concrete including effect of steel fiber,” Indian Concrete Journal, vol. 94, no. 4, pp. 1—9, 2020.
28. P.N. Ojha, A. Trivedi, B. Singh, A. K. N. S, V. Patel, and R.K. Gupta, “High performance fiber reinforced concrete — for repair in spillways of concrete dams,” Research on Engineering Structures and Materials, 2021, doi: 10.17515/resm2021.252ma0128.
29. B Singh, P N Ojha, A Trivedi, V Patel, & V V Arora (2021). Development Of Empirical Equations For Prediction Of Flexural And Split Tensile Strength For Normal And High Strength Concrete With Granite And Calc-Granulite Aggregate, Indian Concrete Journal, November 2021, Vol.95, No.11, pp 36—46.
30. P N Ojha, B Singh, P Kaura, & A Singh “Lightweight geopolymer fly ash sand: an alternative to fine aggregate for concrete production,” Research on Engineering Structures & Materials, 2021.
31. M. Hambach, D. Volkmer, Properties of 3D‑printed fiber-reinforced Portland cement paste, Cement Concr. Compos. 79 (2017) 62—70.
32. L. Pham, P. Tran, J. Sanjayan, Steel fibres reinforced 3D printed concrete: influence of fibre sizes on mechanical performance, Construct. Build. Mater. 250 (2020) 118785.
33. B. Panda, S. Chandra Paul, M. Jen Tan, Anisotropic mechanical performance of 3D printed fiber reinforced sustainable construction material, Mater. Lett. 209 (2017) 146—149.
| Author: A. Trivedi, M.K. Mandre, B. Singh, P.N. Ojha |
| Section: Concrete |
| Keywords: 3D printing, concrete mix, flow, buildability, yield stress, open time |